
 By Walmay
 28 Sep, 2026
 6 Minutes Read
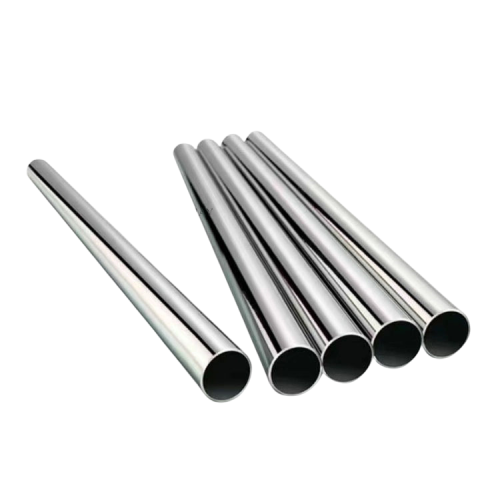
For most pressure applications, welded stainless steel pipe made with modern ERW or double-submerged-arc welding is perfectly adequate and often the smarter buy — the old rule that ‘seamless is always stronger’ hasn’t been true for decades. The real decision comes down to pressure class, pipe diameter, and whether your specification actually mandates seamless construction, not blind tradition.
Here’s an uncomfortable truth for a lot of purchasing managers: the belief that seamless pipe is inherently stronger than welded pipe is mostly outdated thinking from the 1960s, before weld quality control caught up. Today’s high-frequency ERW and automated GTAW longitudinal welds on stainless steel routinely achieve joint efficiencies of 0.9 to 1.0 when properly qualified and tested.
The ASME B31.3 process piping code doesn’t ban welded pipe from pressure service — it applies a weld joint efficiency factor (E) in the pressure calculation. For double-welded pipe with full radiographic examination, E often equals 1.0, meaning no derating at all versus seamless. The myth persists because a lot of buyers never check the actual E factor; they just default to seamless out of habit or because a spec written 20 years ago said so.

The Barlow formula (or its ASME-adjusted version) is what determines whether a pipe can handle your design pressure — and the weld joint efficiency factor is baked directly into that math. A thinner-wall welded pipe with E=1.0 can outperform a thicker seamless pipe that’s undersized elsewhere in the system.
P = (2 × S × t × E) / D, where S is allowable stress, t is wall thickness, E is joint efficiency, and D is outside diameter. Push E from 0.85 (single-welded, spot-radiographed) to 1.0 (double-welded, fully radiographed) and you gain roughly 15% more allowable pressure without changing a single dimension. That’s often enough to make a welded pipe spec work where engineers assumed only seamless would.
| Weld Type | Typical Joint Efficiency (E) |
|---|---|
| Seamless | 1.0 (no factor applied) |
| Double-welded, full RT | 1.00 |
| Double-welded, spot RT | 0.90 |
| Single-welded, no RT | 0.80 |
There are situations where seamless isn’t just preferred, it’s non-negotiable. High-pressure hydraulic lines, small-bore instrumentation tubing under cyclic fatigue, and certain oil & gas wellhead components fall squarely into seamless territory because there’s no weld seam to become a fatigue crack initiation point.
For instance, a hydraulic system operating at 3,000+ PSI with constant pressure cycling will fatigue-crack a welded seam long before it fails the base metal. Seamless pipe under 4 inches NPS is also more readily stocked and machined for tight-tolerance fittings, which matters for instrumentation and control loops where dimensional consistency trumps cost. If your project touches oil and gas material upgrades, expect seamless to be specified by default for critical wellhead and flowline sections.

Large-diameter runs above 12 inches NPS are where welded pipe stops being a compromise and starts being the only sensible option — seamless simply isn’t economical or widely available at that size. Structural pressure vessels, large process lines, and water/utility infrastructure routinely spec welded pipe with full radiographic inspection and get equivalent performance at a lower cost per foot.
Consider a food processing plant expanding a CIP (clean-in-place) distribution loop at 8-inch diameter, moderate pressure around 150 PSI. Specifying seamless here adds cost and extends lead time with zero real performance benefit — a double-welded pipe with E=1.0 handles the load easily and ships faster. Buyers chasing large-bore stock should also check tolerance behavior; see our breakdown on coil tolerances for how upstream strip variation feeds into finished pipe wall consistency.

Picking seamless vs welded is only half the equation — the alloy underneath the construction method determines whether your pipe survives the actual media. A 316L welded pipe handling mild caustic solution will outlast a 304 seamless pipe in the same service, weld type aside.
For chemical processing pressure lines, run the corrosion analysis before the construction-method debate. Our comparison on 304 vs 316 stainless steel and the deeper dive into 904L for aggressive chemical service both matter more to pipe longevity than whether the seam is welded or absent. Get the grade wrong and no amount of seamless construction saves you from pitting corrosion at the weld heat-affected zone or anywhere else.
Seamless pipe typically runs 15-30% higher per foot than equivalent welded pipe in the same grade and schedule — the gap widens further as diameter increases, since seamless manufacturing gets exponentially harder above 8 inches. For a 500-foot run of 6-inch Schedule 40 316L pipe, that difference can easily add five figures to a project budget with no corresponding gain in pressure capacity if the welded spec already meets E=1.0.
Seamless pipe in less common sizes or wall schedules often means longer mill lead times because it’s produced in batch runs, not continuous coil-fed lines. Welded pipe, by contrast, can often be produced faster from stock strip or coil — something worth checking against your project schedule before locking in a seamless-only spec.

The table below summarizes the practical tradeoffs procurement teams weigh most often when specifying pressure pipe.
| Criteria | Seamless Pipe | Welded Pipe (ERW/Fusion) |
|---|---|---|
| Manufacturing method | Extruded/drawn from solid billet | Rolled strip, longitudinally welded |
| Wall thickness consistency | Can vary ±12.5% (ASTM A999) | Tighter, more uniform ±10% |
| Pressure rating (equal OD/wall) | Baseline, no weld factor | Requires joint efficiency factor (0.85-1.0) |
| Typical cost | 15-30% higher | Lower, especially in large diameters |
| Availability in large OD | Limited above 12 inch | Readily available up to very large OD |
| Inspection/traceability | No weld seam to inspect | Weld seam requires NDT/RT |
| Best use case | High-pressure, small-bore, critical service | Mid-pressure, large-bore, budget-conscious runs |
| Corrosion at seam | No seam-related risk | Possible if weld/HAZ not passivated properly |
ASTM A312 covers both seamless and welded stainless pipe for corrosive and high-temperature service, while ASTM A358 and A409 handle larger welded pipe specifically for pressure applications. Don’t let a vague purchase order leave the construction method ambiguous — specify the exact standard, schedule, and grade, or you risk receiving whichever the mill has on hand.
Also confirm whether your project spec requires 100% radiographic testing (RT) or just spot RT on welded pipe — this single line item changes the joint efficiency factor and therefore the allowable pressure rating. If you’re comparing this against related product decisions, our guide on pipes vs tubes covers a different but related sourcing question worth checking before finalizing your order.
 Industry Knowledge
 Industry Knowledge
 Industry Knowledge
Walmay will help match the right stainless product form and specification for your application, confirm quantities and packing needs, and provide requested documents based on order requirements.